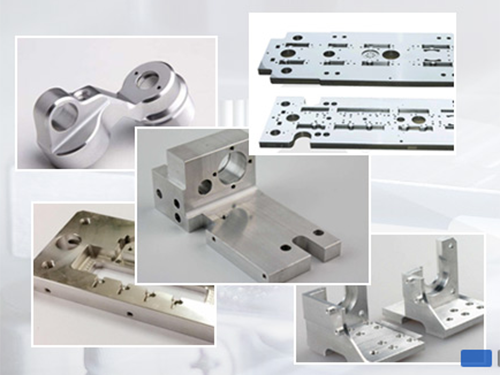
Improving the surface finish of stainless steel precision parts during machining is influenced by many factors, including the lathe, the material, and the cutting tools. General machine tools can achieve Ra 1.6, while high-speed precision machine tools for machining aluminum can achieve Ra 0.2. The surface finish of parts with patterns will be compromised.
The main problem here is that the wrinkles on the parts are difficult to handle, and there are many factors involved. If it is a long shaft, it may be that the tailstock force is insufficient, or the tailstock is moving. If there is no problem with the tailstock, it may be due to tool wear, machining parameters, cutting fluid, and many other issues.
Another factor is the material used in machining precision stainless steel parts, and the corresponding choice of cutting tools. Furthermore, there are issues with the machine tool itself, which can only be resolved through practical experience. However, these factors alone are insufficient; other reasons need to be explored.
The main reason is actually the machining strength of stainless steel precision parts. It could be that the protruding length of your part is too long, or that your cutting tool is too long. The center of gravity of the cutting tool might also be too high. Choosing a suitable cutting tool is necessary. Sometimes, excessively high rotation speeds can cause resonance between the machine tool and the workpiece/cutting tool, which can also result in patterns.
First, ensure the lathe's stability, specifically its secure mounting. Next, check for vibrations during high-speed spindle operation. Coolant is crucial. Then, ensure your cutting tools are properly sharpened, and that the chip vents are well-designed to prevent chip damage to the workpiece. When chamfering the cutting tool, create rounded corners. Finally, avoid holding the tool in place during installation.
It's about matching the spindle speed and the feed rate. If your lathe isn't working well, I suggest buying some sandpaper and fixing it. When sanding, I recommend adjusting it according to the working direction of the cutting tool. This will make the texture of the stainless steel precision parts look better.